

- Site Navigation -
Idler Roller Manufacturer OEM and Custom Solutions Guide
Author:yuexing Date:2026-09-17 22:16:55 Hits:138
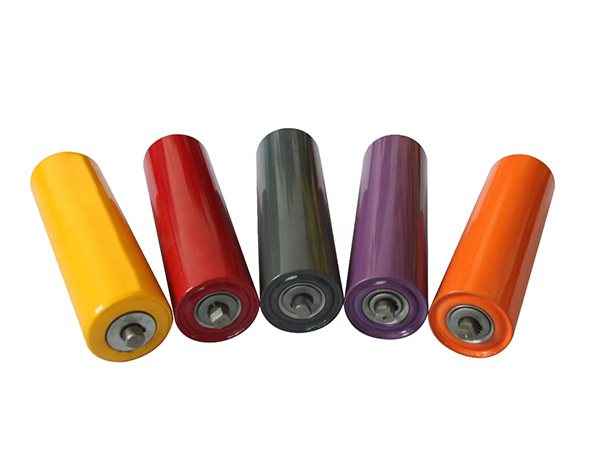
The difference between buying an idler from a catalogue and working with an idler roller manufacturer on a custom or OEM basis is the difference between buying a part and designing a solution. A catalogue transaction is straightforward: the buyer selects a standard product, pays the listed price, and receives something that was designed for the average case. An OEM or custom engagement involves sharing information about the actual application, the duty conditions, and the performance targets — and receiving in return a product that is designed for the specific situation rather than the generic one. Done well, that engagement produces idlers that last longer, fit better, and generate fewer unplanned stoppages than catalogue equivalents. Done poorly, it produces delays, specification arguments, and products that still do not perform as expected. This guide is about doing it well.
What OEM Means for Idler Rollers
OEM (Original Equipment Manufacturer) in the context of idler roller manufacturer relationships usually means one of two things. The first is private-label supply: a manufacturer produces idlers to a buyer's specification and the buyer sells them under their own brand. This is common in the conveyor equipment distribution channel, where distributors want to offer an own-brand product without investing in manufacturing capability. The second OEM variant is component supply to an OEM equipment builder: a manufacturer supplies idlers as part of a new conveyor system build, where the idler specification is set by the system designer and the manufacturer must meet the designer's performance requirements.
In both cases, the OEM idler roller manufacturer relationship is characterised by volume commitments, extended supply agreements, and a degree of specification ownership that does not exist in spot-purchase transactions. The manufacturer needs to understand the volume trajectory and product lifecycle to justify tooling investments; the buyer needs quality consistency across production batches that a spot supplier does not guarantee. These requirements are best handled through a formal supply agreement that specifies not just unit price but quality standards, defect rates, delivery commitments, and what happens when the specification is not met.
The Custom Design Process from the Manufacturer's Side
When a buyer approaches an idler roller manufacturer with a non-standard requirement — a non-standard diameter, a high-temperature service condition, a specific material incompatibility to resolve — the manufacturer's internal process for handling that brief has a predictable sequence. The first stage is technical review: the manufacturer assesses whether the requirement is achievable within their manufacturing capability and whether the quantities and timeline are realistic. If the requirement involves new tooling, the manufacturer calculates the tooling cost and the unit price structure with and without that cost amortised.
The second stage is a technical exchange: the manufacturer asks questions about the application that may not have been in the original brief. The operating temperature, the material being handled, the belt speed, the loading pattern, the environment — these details determine the correct specification and are the difference between a product that works and one that appears to work until it does not. A manufacturer who provides a quote without asking about the application is selling a standard part with a custom description; one who asks detailed questions is engaging with the problem.
The third stage is a formal specification: the manufacturer produces a technical data sheet or drawing that defines the product to be manufactured, including all dimensions, material grades, surface treatments, and performance parameters. The buyer reviews and approves this document before production begins. This specification is the contract between buyer and manufacturer — it is what the product must meet and what the buyer can hold the manufacturer to. A custom order that proceeds without a signed specification is a dispute waiting to happen.
What to Look for in an Idler Roller Manufacturer
The first thing to verify is whether the idler roller manufacturer actually manufactures what they sell, rather than sourcing from a third-party factory and relabelling it. The practical test is to ask to visit or photograph the production line and to ask specific technical questions about their process: how they hold shaft tolerance, how they treat frames after welding, how they test finished idlers. A manufacturer can answer these questions; a trader cannot. This distinction matters because a manufacturer has direct control over quality and can respond to specification issues; a trader can communicate but cannot compel.
Second, assess their quality system. Ask whether they operate to a documented quality management standard — ISO 9001 is the minimum, and it is not difficult to achieve, so the absence of any quality management system documentation is a signal worth noting. Ask about their defect rate and how they handle it. A manufacturer who tracks defect rates, investigates root causes, and feeds that information back into their process is fundamentally different from one who replaces defective units without analysing why.
Third, assess their technical capability for custom work. Ask about their in-house machining, fabrication and testing capability. A manufacturer who outsources shaft machining to a third party is dependent on that supplier's quality and lead times for any custom dimension or tolerance. One who machines shafts in-house can respond to specification changes quickly and control the critical tolerances directly. This distinction matters most for custom and OEM work, where specification changes during a production run are more common than in standard catalogue production.
Structuring a Long-Term Supply Agreement
The unit price is the least important term in a long-term OEM supply agreement. The terms that matter are quality standards (what defect rate triggers a corrective action), delivery commitments (lead time, on-time performance requirements, and what happens when they miss it), specification change management (how changes to the product specification are handled, priced, and implemented), and continuity provisions (what happens if the manufacturer cannot supply — who owns the tooling, can the buyer transfer it to another manufacturer). A buyer who negotiates only on unit price and accepts whatever lead time the manufacturer offers is giving up the terms that actually protect their operations.
Volume commitments are the other key term. An idler roller manufacturer investing in tooling for a custom product needs volume commitment to justify the investment. The buyer needs protection if their volume does not materialise. A typical compromise is a minimum order quantity commitment for the initial production run, with annual volume forecasts for subsequent periods and a mechanism to adjust the unit price if actual volumes deviate significantly from forecast. This structure protects both parties: the manufacturer has the volume signal to justify investment, and the buyer is not locked into a volume that does not materialise.
Managing the Custom Product Development Timeline
Custom idler development timelines are often underestimated by buyers who are accustomed to ordering from stock. The typical sequence for a moderately complex custom idler roller manufacturer engagement — a new frame geometry, non-standard shell diameter — runs approximately as follows: technical brief and specification development, 2–3 weeks; tooling and first article production, 4–6 weeks; first article inspection and approval, 1–2 weeks; production ramp and first delivery, 2–4 weeks. Total elapsed time from brief to first delivery, 9–15 weeks for a non-trivial custom product. Designs that involve new roller tube tooling or non-standard bearing arrangements can run longer. A buyer who plans their conveyor shutdown schedule around a 3-week delivery expectation for a custom product will be disappointed.
FAQ
What is the difference between an OEM idler roller manufacturer and a distributor?
An OEM manufacturer produces the idler — they control the design, the manufacturing process, the quality, and the component sourcing. A distributor buys finished idlers from a manufacturer and resells them, typically adding logistics, warehousing and sometimes after-sales support. The distinction matters because a distributor cannot fix a manufacturing quality problem — only the manufacturer can. For custom and OEM work, only the actual manufacturer can develop and produce the product; a distributor can facilitate the relationship but cannot replace it.
How long does custom idler roller manufacturer development take?
For a non-standard diameter or length on an existing frame design, 4–6 weeks from specification approval to first article. For a new frame geometry, 8–12 weeks from specification approval to first article. For fully bespoke idlers with new tooling for the roller shell and frame, 12–18 weeks is realistic. These are approximate ranges and depend on the complexity of the custom requirement and the manufacturer's current workload.
What quality standards should an idler roller manufacturer meet?
ISO 9001 is the minimum. Beyond that, look for manufacturers who can provide first article inspection reports with each delivery, batch-level material traceability for the bearing and shaft steel, and a documented non-conformance and corrective action process. For food-grade or high-temperature applications, the manufacturer should have relevant third-party certifications for the applicable environment.
Can an idler roller manufacturer produce replacement idlers for an obsolete model?
Yes, through reverse engineering. Provide the original idler or a detailed dimensioned drawing, and the manufacturer can reverse engineer the components and produce a functionally equivalent replacement. This is particularly valuable for idlers on older conveyors where the original manufacturer no longer supports the product line. Lead time for reverse-engineered replacements is typically 4–8 weeks depending on complexity.
Conclusion
The idler roller manufacturer relationship works best when it is treated as a partnership rather than a procurement transaction. The buyer who shares application details, approves specifications before production, and structures supply agreements that protect both quality and continuity gets better outcomes than one who buys on unit price alone. The manufacturer who asks about the application, provides clear technical documentation, and maintains a documented quality system is the partner worth building a long-term relationship with. That relationship pays dividends in the form of consistent quality, responsive custom development, and fewer unplanned stoppages over the life of the conveyor.
References
Conveyor Equipment Manufacturers Association. CEMA 7th Edition — Belt Conveyors for Bulk Materials. CEMA, 2014.
Molnár, V., Fedorko, G., Stehlíková, B., et al. "A Failure Analysis of Idler Rolls of Belt Conveyors." Engineering Failure Analysis, vol. 45, 2014, pp. 155-165.
Harrison, A. "Determining the Life of Conveyor Rollers Using Fatigue Theory." Bulk Solids Handling, vol. 25, no. 5, 2005, pp. 290-295.
Zhang, Y., Yang, X., and Meng, L. "Review of Belt Conveyor Idler Roller Research." Mining Science and Technology, vol. 33, no. 3, 2023, pp. 415-428.
Contact Us
Tel:8615031765579
WhatsApp:+8615031765579
E-mail:905675277@qq.com
Add:Likou Village, Chenzhuang Town, Xian County, Hebei Province, China
Url:https://www.yxidlerrollers.com