

- Site Navigation -
Conveyor Idler Maintenance Best Practices and Inspection Guide
Author:yuexing Date:2026-08-30 12:58:48 Hits:53
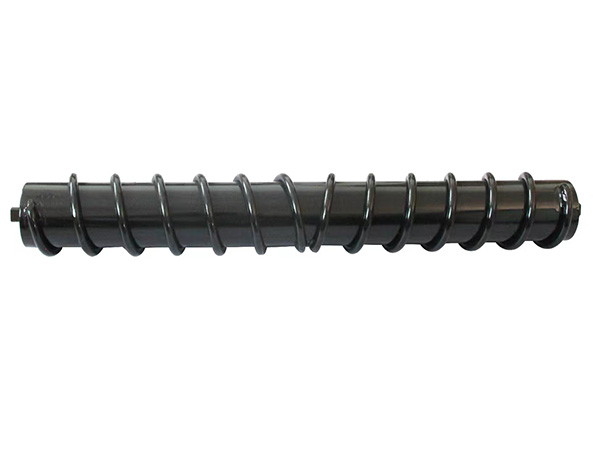
There is a simple test for whether a plant's conveyor idler maintenance programme is working: look at the distribution of idler ages on the conveyor. In a well-run plant, idler ages cluster around two or three groups — the ones replaced during scheduled shutdowns at the expected life interval, and the ones replaced reactively between shutdowns because something genuinely unexpected happened. In a poorly-run plant, idler ages are randomly distributed across a wide range, which means some idlers that failed at 8,000 hours were replaced while identical idlers at 40,000 hours are still running — a sign that failures are being caught by chance rather than by inspection, and that the maintenance programme is not actually measuring what it thinks it is measuring. This guide covers the inspection practices, replacement criteria, and organisational habits that make a conveyor idler maintenance programme work in practice rather than on paper.
Setting Inspection Frequency by Criticality and Environment
Not every conveyor needs the same inspection frequency. A conveyor running at 6 m/s with 6,000 tonnes per hour throughput in an iron ore port justifies daily visual inspection. A conveyor moving low-speed aggregate in a dry quarry interior can run on weekly visual checks with monthly detailed inspections. The key is matching the inspection interval to the consequence of failure: a conveyor whose failure stops a production process worth 500,000 dollars per day of throughput needs more frequent monitoring than one whose failure stops a section that can be bypassed or stockpiled.
For most plant contexts, we recommend a tiered inspection schedule: a weekly visual walk-by that checks for obvious abnormalities like excessive vibration, visible bearing protrusion, or belt mistracking; a monthly detailed inspection that includes temperature measurement at bearing positions using a contact or infrared thermometer, with any position reading more than 15 degrees Celsius above ambient flagging for closer monitoring; and a quarterly inspection that includes a full bearing condition assessment on a sample of idlers from representative stations across the run. Temperature and vibration trending over time is far more useful than a single reading — a bearing that runs at 60 degrees consistently for six months is usually fine; one that runs at 50 degrees and then climbs to 68 degrees over two weeks is not.
Visual Inspection: What to Look For and What to Ignore
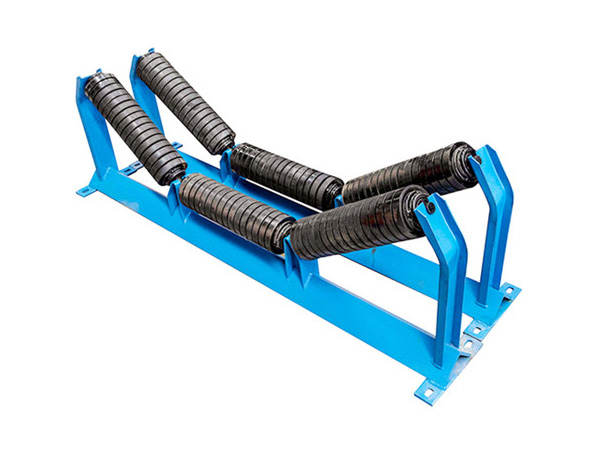
A trained eye can catch most developing conveyor idler maintenance problems during a walk-by inspection without touching the equipment. The key indicators are: abnormal vibration felt through the structure or heard audibly as a knock or rumble, which usually indicates a bearing in the early stages of degradation before seizure; visible shell damage — gouges, punctures, or deformation that indicates impact damage or severe abrasion; material accumulation on the shell or frame that suggests carryback or spillage, which creates an eccentric load that accelerates bearing wear; belt mistracking at a specific position that consistently repeats at the same idler station; and frame distortion or mounting bolt loss that indicates structural movement. None of these require tools to detect, but they do require the inspector to know what they are looking at and to report it clearly to whoever makes the replacement decision.
The most common inspection error is looking for the wrong things. A cracked shell that is not leaking material is not a conveyor idler maintenance priority; a bearing running 20 degrees hot is. Minor shell scoring from normal abrasion is expected; a shell that has worn through to the point where material can reach the bearing cavity is a critical replacement. The distinction matters because over-maintaining idlers — replacing components that still have life — wastes budget and creates unnecessary downtime, while under-maintaining them allows preventable failures to cascade into belt damage and structural problems.
Replacement Criteria: When to Change an Idler
Replacing idlers on a fixed calendar schedule — every 30,000 hours regardless of condition — is better than doing nothing, but it leaves significant value on the table because it replaces idlers that still had life and leaves in service idlers that are already degrading. The better approach is condition-based replacement guided by inspection findings and operational data. The specific triggers for replacement are: bearing temperature more than 20 degrees Celsius above ambient at the measurement point, with confirmation by repeat measurement on a cool conveyor after a shutdown; audible knocking or rumbling that is new and persistent, not intermittent; visible bearing seal failure with lubricant weeping from the bearing housing; shell wear that has reduced the roller diameter by 15% or more from nominal; any shell puncture or damage that allows material to reach the bearing cavity; and frame distortion that prevents proper belt alignment even after realignment attempts.
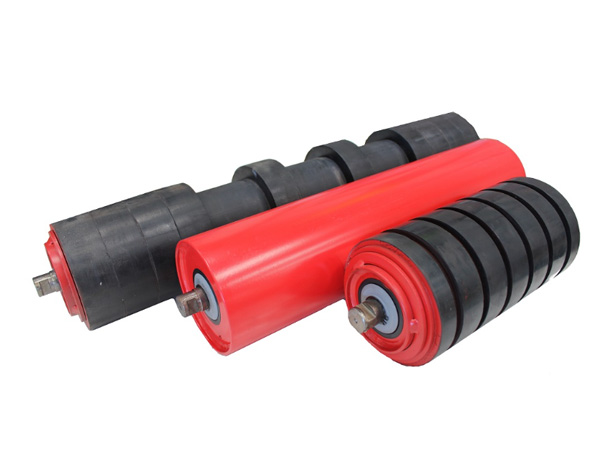
Loading zone impact idlers have a separate replacement criterion because their duty cycle is harsher. The rubber or polymer cushioning elements degrade over time from repeated compression cycles, and their effectiveness in absorbing impact energy reduces long before the shell or bearing shows visible damage. The practical trigger for impact idler replacement is a reduction in the shell wall thickness at the impact zone of 20% or more from nominal, measured with a ultrasonic wall thickness gauge during a scheduled shutdown, or any visible compression set in the cushioning elements where the polymer has permanently deformed and no longer returns to its original shape.
Lubrication Practice for Sealed and Relubricatable Bearings
The majority of modern idler bearings are sealed-for-life designs — the bearing is packed with grease at the factory, the seals prevent contamination ingress, and the bearing is not intended to be relubricated during its service life. For these sealed bearings, conveyor idler maintenance practice is straightforward: do not add lubricant. Attempting to relubricate a sealed bearing with a grease gun will over-pressure the seal and force grease out or contamination in, shortening life rather than extending it. The only maintenance action required is to verify the seals are intact during visual inspection.
For relubricatable bearings — typically specified in heavy-duty or high-temperature applications where the operating temperature exceeds the rating of sealed-for-life greases — the lubrication interval is determined by operating temperature and contamination level. As a starting point, relubrication every 2,000–3,000 operating hours at normal temperatures is conservative. The relubrication interval should be adjusted based on bearing temperature trending: if the bearing runs consistently cool (within 10 degrees of ambient), the interval can be extended; if it runs above 70 degrees Celsius at the housing, the interval should be shortened and the grease type reviewed. Over-greasing is as damaging as under-greasing for rolling element bearings — the correct practice is to add grease slowly until a small amount is seen to purge from the seal, then stop.
Alignment Checking and Trough Profile Verification
Belt mistracking that appears at a specific position is often a trough profile problem at that idler set rather than a belt or structure problem elsewhere. The check is simple: with the conveyor stopped, measure the trough angle of the centre roll and both side rolls against the design specification using an angle finder or digital protractor. Cumulative installation error — where each idler in a run is set 0.5 degrees off in the same direction — can accumulate into a significant total deviation over a long conveyor, producing a consistent mistracking tendency that training idlers cannot fully correct. The corrective action for cumulative error is systematic resurvey and reset, not adding more training idlers to compensate.
A trough profile check should be part of every scheduled shutdown inspection on critical conveyors, not just when mistracking is observed. The time investment is 5–10 minutes per idler set and it catches alignment drift before it creates belt edge damage or accelerates bearing loads on the affected idlers. The conveyor idler maintenance record should log the measured trough angles so that drift over time is visible — if a given idler set is consistently measuring 1–2 degrees off the design angle at every shutdown inspection, the mounting hardware or frame is degrading and needs structural attention, not just realignment.
Staff Training and Reporting Habits
The best inspection schedule is worthless if the person doing the inspection does not know what to look for, does not have a clear reporting path for findings, and does not see follow-up action taken on their reports. Training for conveyor idler maintenance inspectors should cover the four most common failure indicators — abnormal vibration, elevated temperature, shell damage, and mistracking — and the specific language to use when reporting each finding. A report that says "idler 47 on carry section B is making a noise" is less useful than one that says "idler 47 on carry section B is running with a rhythmic knocking audible from 3 metres, temperature 12 degrees above ambient, recommend replacement at next scheduled shutdown or monitoring frequency increased to daily." The second report drives a decision; the first creates an argument.
Maintenance records should capture the age and condition of every replaced idler — the operating hours at replacement and the apparent failure mode. That data is what allows a plant to move from calendar-based replacement to condition-based replacement over time. A plant that has recorded that its idlers consistently fail at 28,000–35,000 hours in a particular position on a particular conveyor can target that position for condition monitoring and extend the replacement interval for the positions where idlers are consistently running to 45,000–55,000 hours without increasing failure risk. That is the data-driven step that separates excellent conveyor idler maintenance from adequate conveyor idler maintenance.
FAQ
How often should conveyor idler maintenance inspections be carried out?
Weekly visual walk-bys for all conveyors, monthly detailed inspections with temperature measurement for high-throughput or critical conveyors, and quarterly full inspections including trough profile checks for the most critical runs. Adjust the frequency up for conveyors in severe environments (heavy dust, coastal, underground) and down for slow, low-throughput, non-critical conveyors. The key is matching the inspection intensity to the consequence of failure.
Should I relubricate sealed-for-life idler bearings?
No. Sealed-for-life bearings are packed with grease designed to last the bearing's service life. Adding grease with a grease gun will over-pressure the seals, forcing lubricant out and potentially drawing contamination in. Leave them sealed and verify the seals are intact during visual inspection.
What is the most cost-effective way to reduce idler-related unplanned downtime?
Condition-based replacement guided by temperature and vibration monitoring. A conveyor that switches from calendar-based replacement to condition-based replacement typically reduces idler-related unplanned stoppages by 25–40% and simultaneously reduces unnecessary idler replacements by 20–30%, because idlers that still had life are no longer being replaced on a fixed schedule.
How do I know when an impact idler needs replacement?
The cushioning elements lose effectiveness before the shell or bearing shows damage. Measure the shell wall thickness at the impact zone with an ultrasonic gauge — replace when wall thickness has reduced by 20% or more from nominal. Visually inspect the cushioning elements for permanent compression set, where the polymer has not returned to its original shape after unloading. Any visible permanent deformation in the cushioning elements is a replacement trigger.
Conclusion
Conveyor idler maintenance works when it is proportionate, data-driven, and connected to a decision. The right programme inspects at frequencies matched to consequence of failure, replaces on condition rather than calendar, logs the data that makes future decisions smarter, and trains the people doing the work to report clearly and see their reports acted on. Plants that do this consistently outperform their peers on idler-related uptime not because they maintain more aggressively, but because they maintain more intelligently — catching the failures that matter early and leaving alone the idlers that still have life.
References
Conveyor Equipment Manufacturers Association. CEMA 7th Edition — Belt Conveyors for Bulk Materials. CEMA, 2014.
Molnár, V., Fedorko, G., Stehlíková, B., et al. "A Failure Analysis of Idler Rolls of Belt Conveyors." Engineering Failure Analysis, vol. 45, 2014, pp. 155-165.
Harrison, A. "Determining the Life of Conveyor Rollers Using Fatigue Theory." Bulk Solids Handling, vol. 25, no. 5, 2005, pp. 290-295.
Fedorko, G., and Molnár, V. "Determination of the Idler Rollers Bearing Load." Research in Engineering, vol. 22, 2013, pp. 45-52.
Contact Us
Tel:8615031765579
WhatsApp:+8615031765579
E-mail:905675277@qq.com
Add:Likou Village, Chenzhuang Town, Xian County, Hebei Province, China
Url:https://www.yxidlerrollers.com